A controlled path from approved drawing to site installation.
Design release, production planning, traceable fabrication, inspection, packing, and site handoff are connected as one project workflow.
Fifteen connected stages, with clear control points.
The sequence shown here follows the aluminium formwork workflow documented in the Schach catalogue. Product-specific operations vary for MS systems and safety screens.
- 01
Approved engineering release
BOQ and fabrication drawings are released after design review and client approval.
- 02
Production planning
PPC prepares raw-material nesting, machine loading, and the production sequence.
- 03
Incoming material inspection
Dimensions and chemical properties are checked lot by lot before production.
- 04
Barcode generation
A unique barcode is assigned for identification and tracking through multiple stages.
- 05
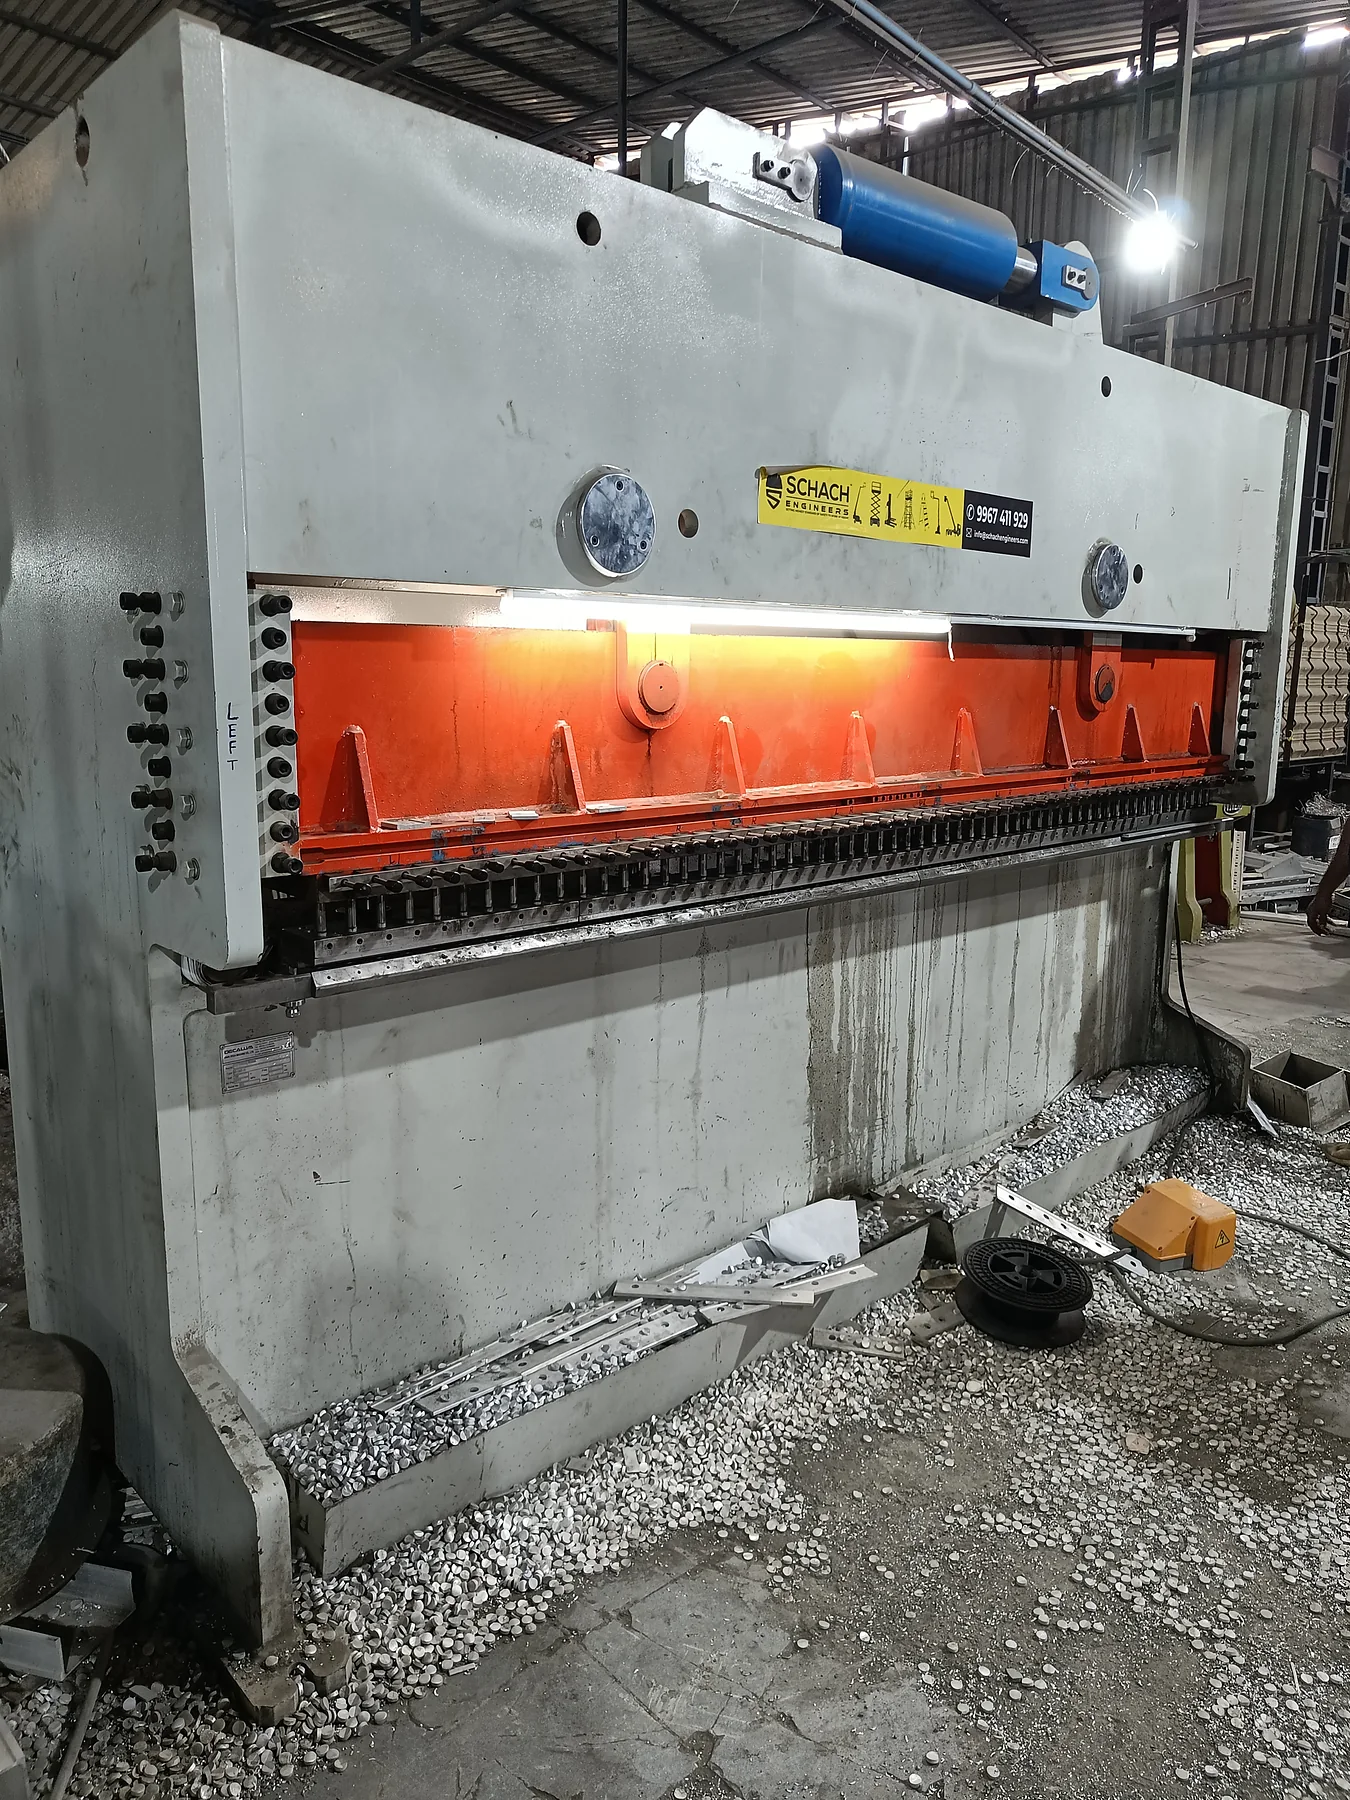
Cutting and shearing
Profiles and sheets are cut to the approved plan and tagged for the next operation.
- 06
Punching and milling
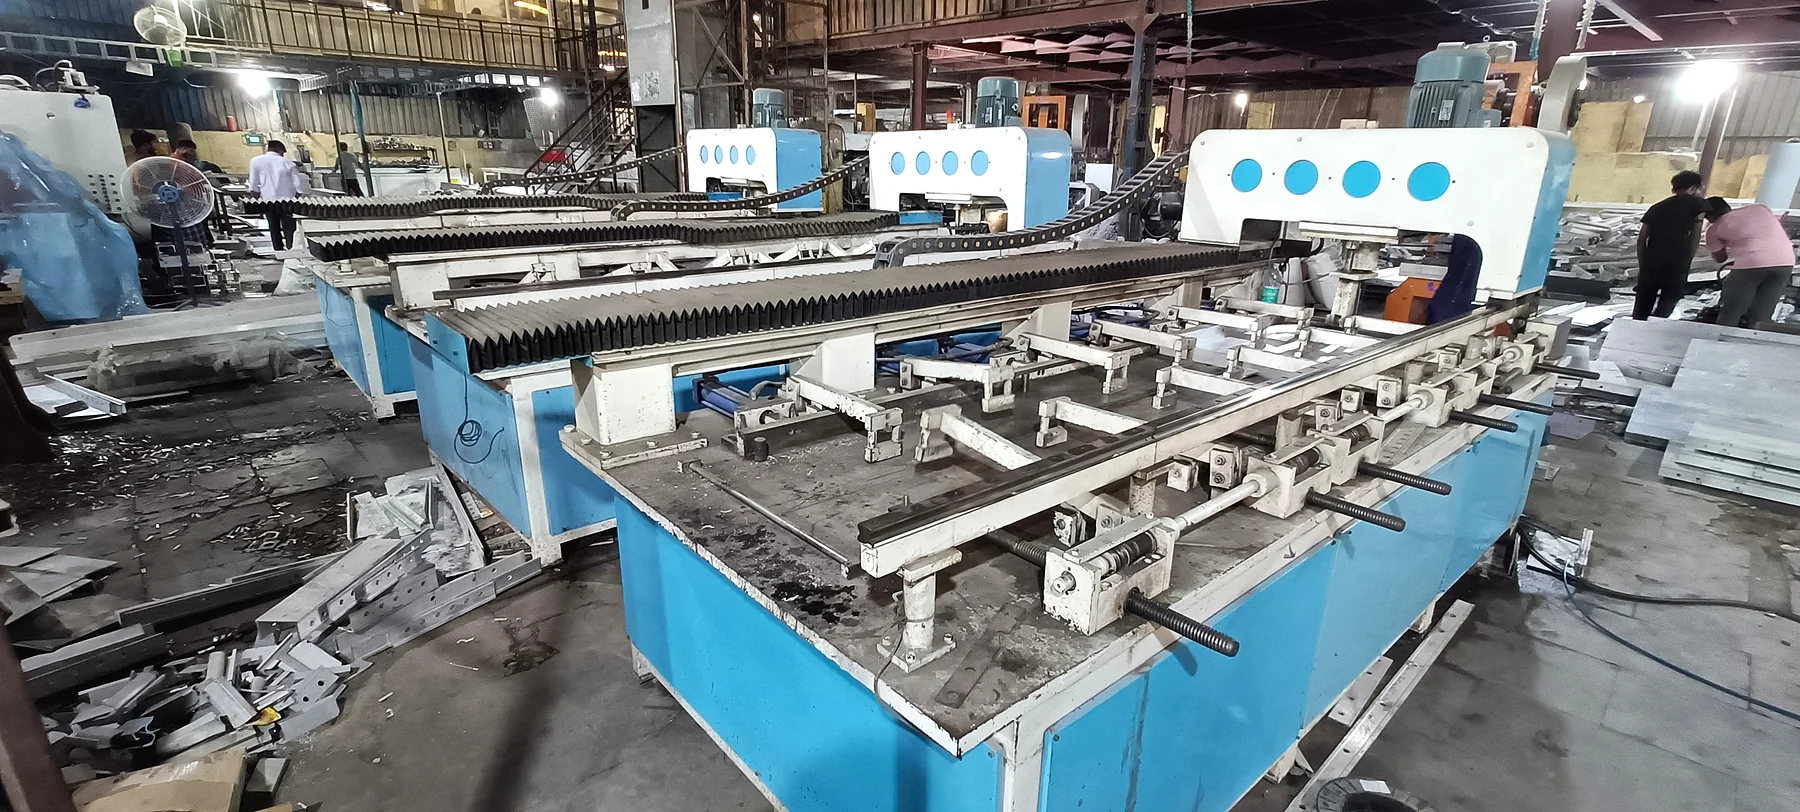
Connection, tie, and edge details are machined to fabrication requirements.
- 07
Friction stir welding
Automated friction welding is used for applicable aluminium panel operations.
- 08
WIP issue and fitting
Components, stiffeners, and assemblies are issued and fitted against drawings.
- 09
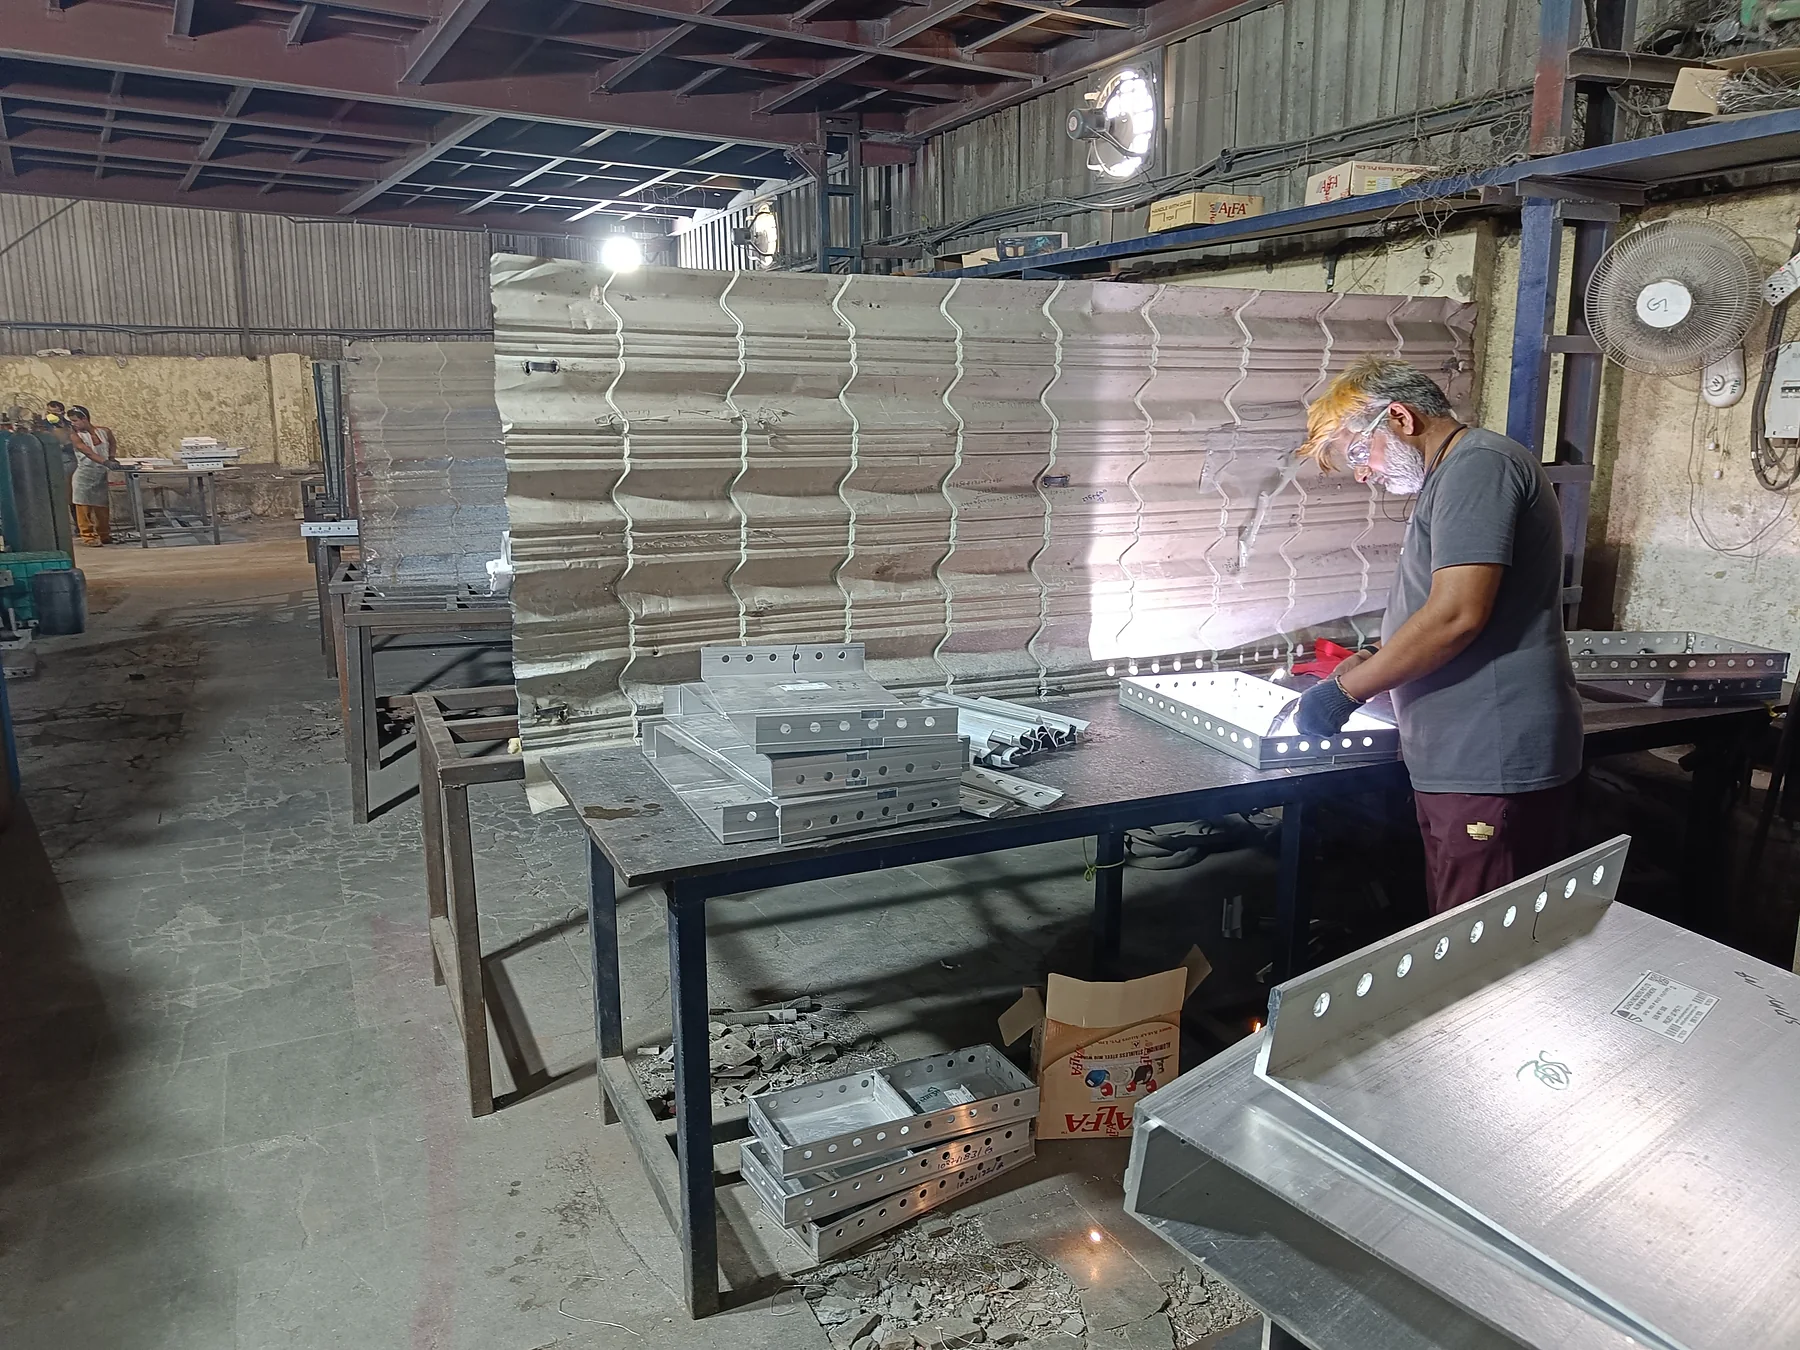
Full welding
Panels and special assemblies move through controlled fabrication and welding lines.
- 10
Grinding and cleaning
Welds and surfaces are prepared, including acid cleaning where specified.
- 11
Final quality inspection
Finished components undergo a documented 100% inspection before finishing.
- 12
Buffing and lacquering
Applicable aluminium surfaces are finished and protected for dispatch and use.
- 13
Mock-up when required
Project-specific assemblies can be trial fitted before bulk site installation.
- 14
Pallet packing
Panels are packed unit wise with identification and a corresponding packing list.
- 15
Dispatch and site handoff
Material reaches site with scanning support and installation verification.
Equipment supports the drawing, not the other way around.
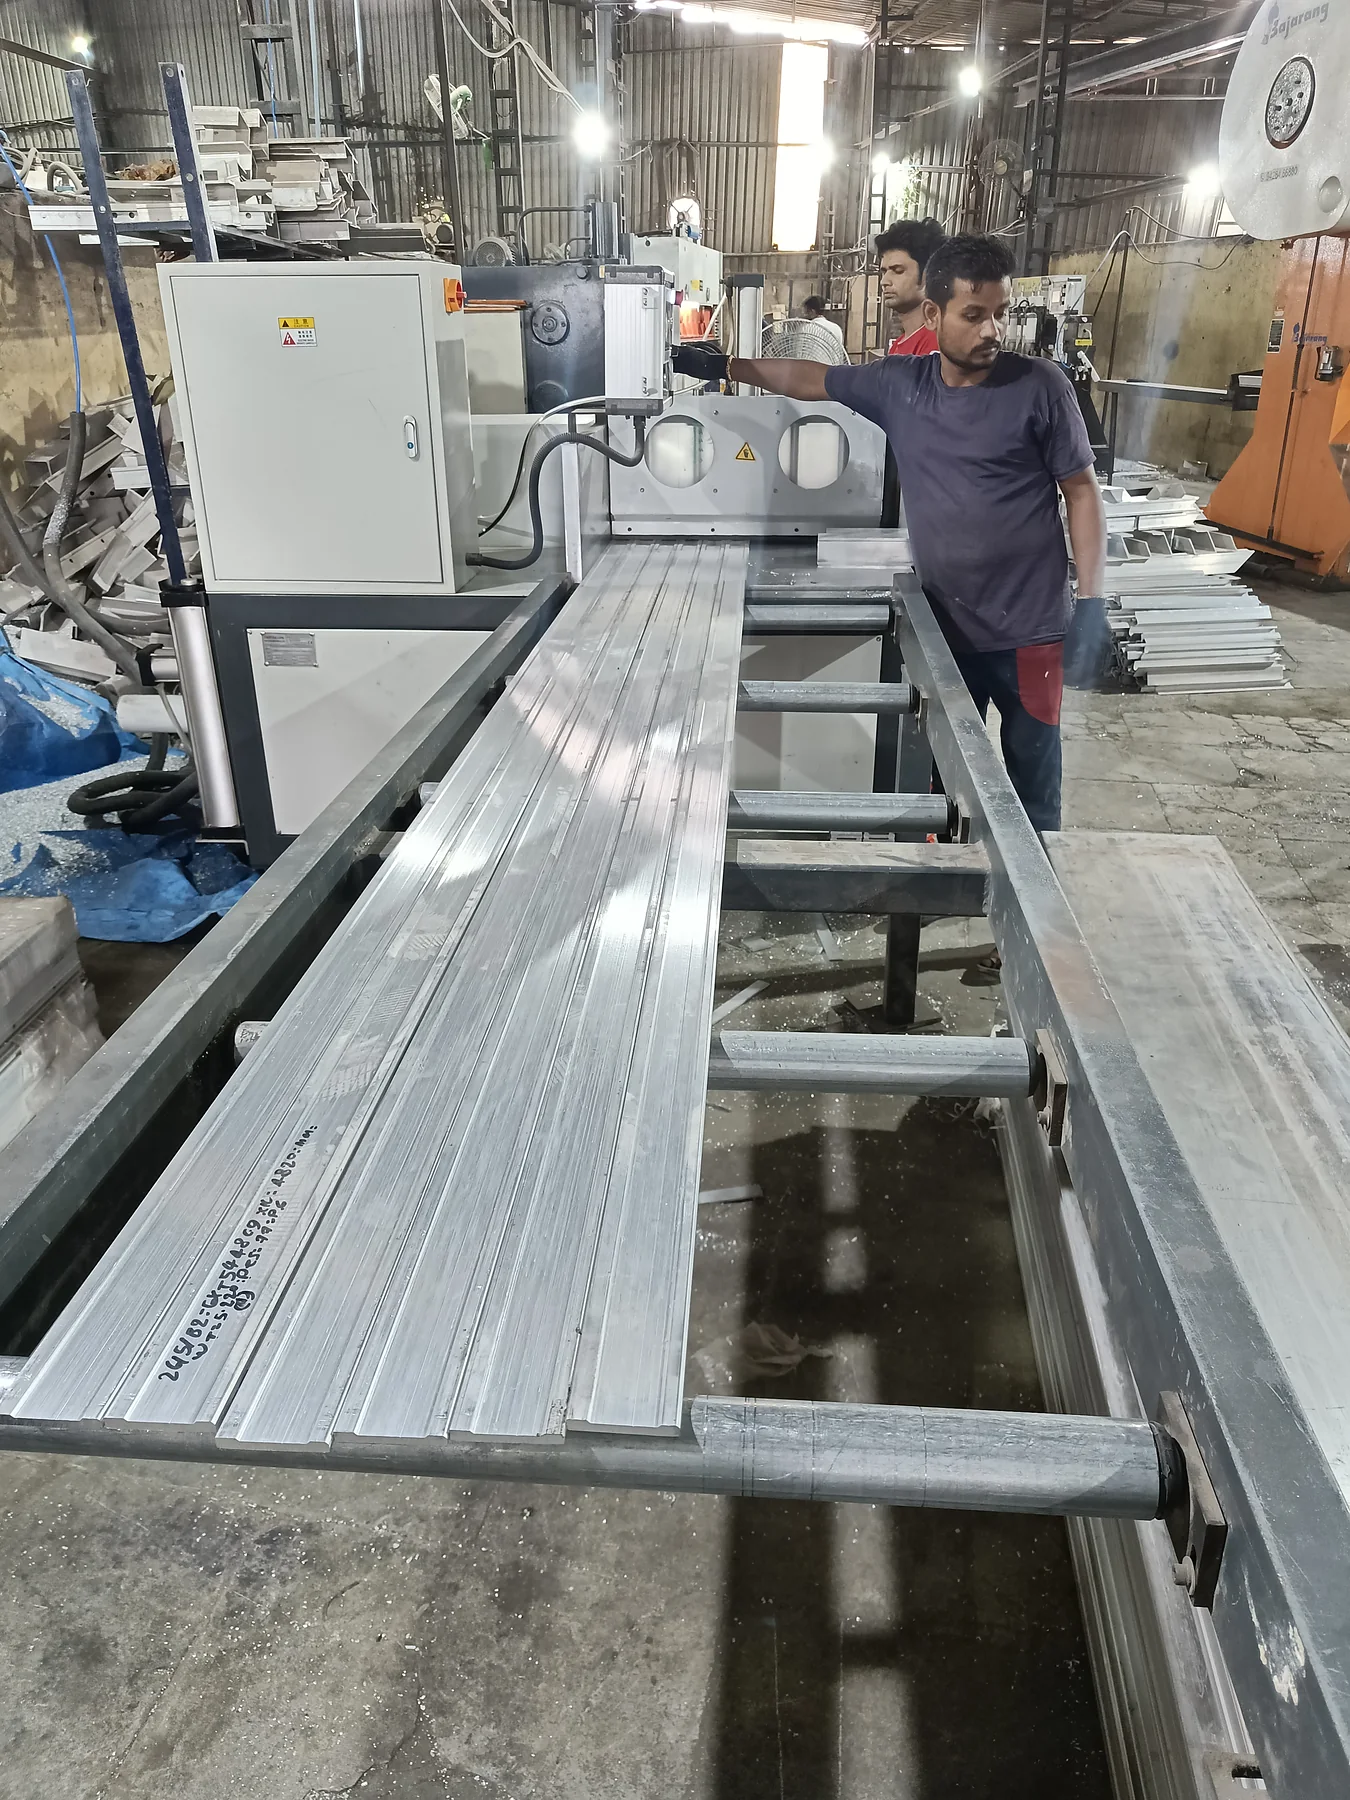
CNC cutting and plasma
Planned profile cutting and CNC plasma operations for repeatable component preparation.
Press shop and shearing
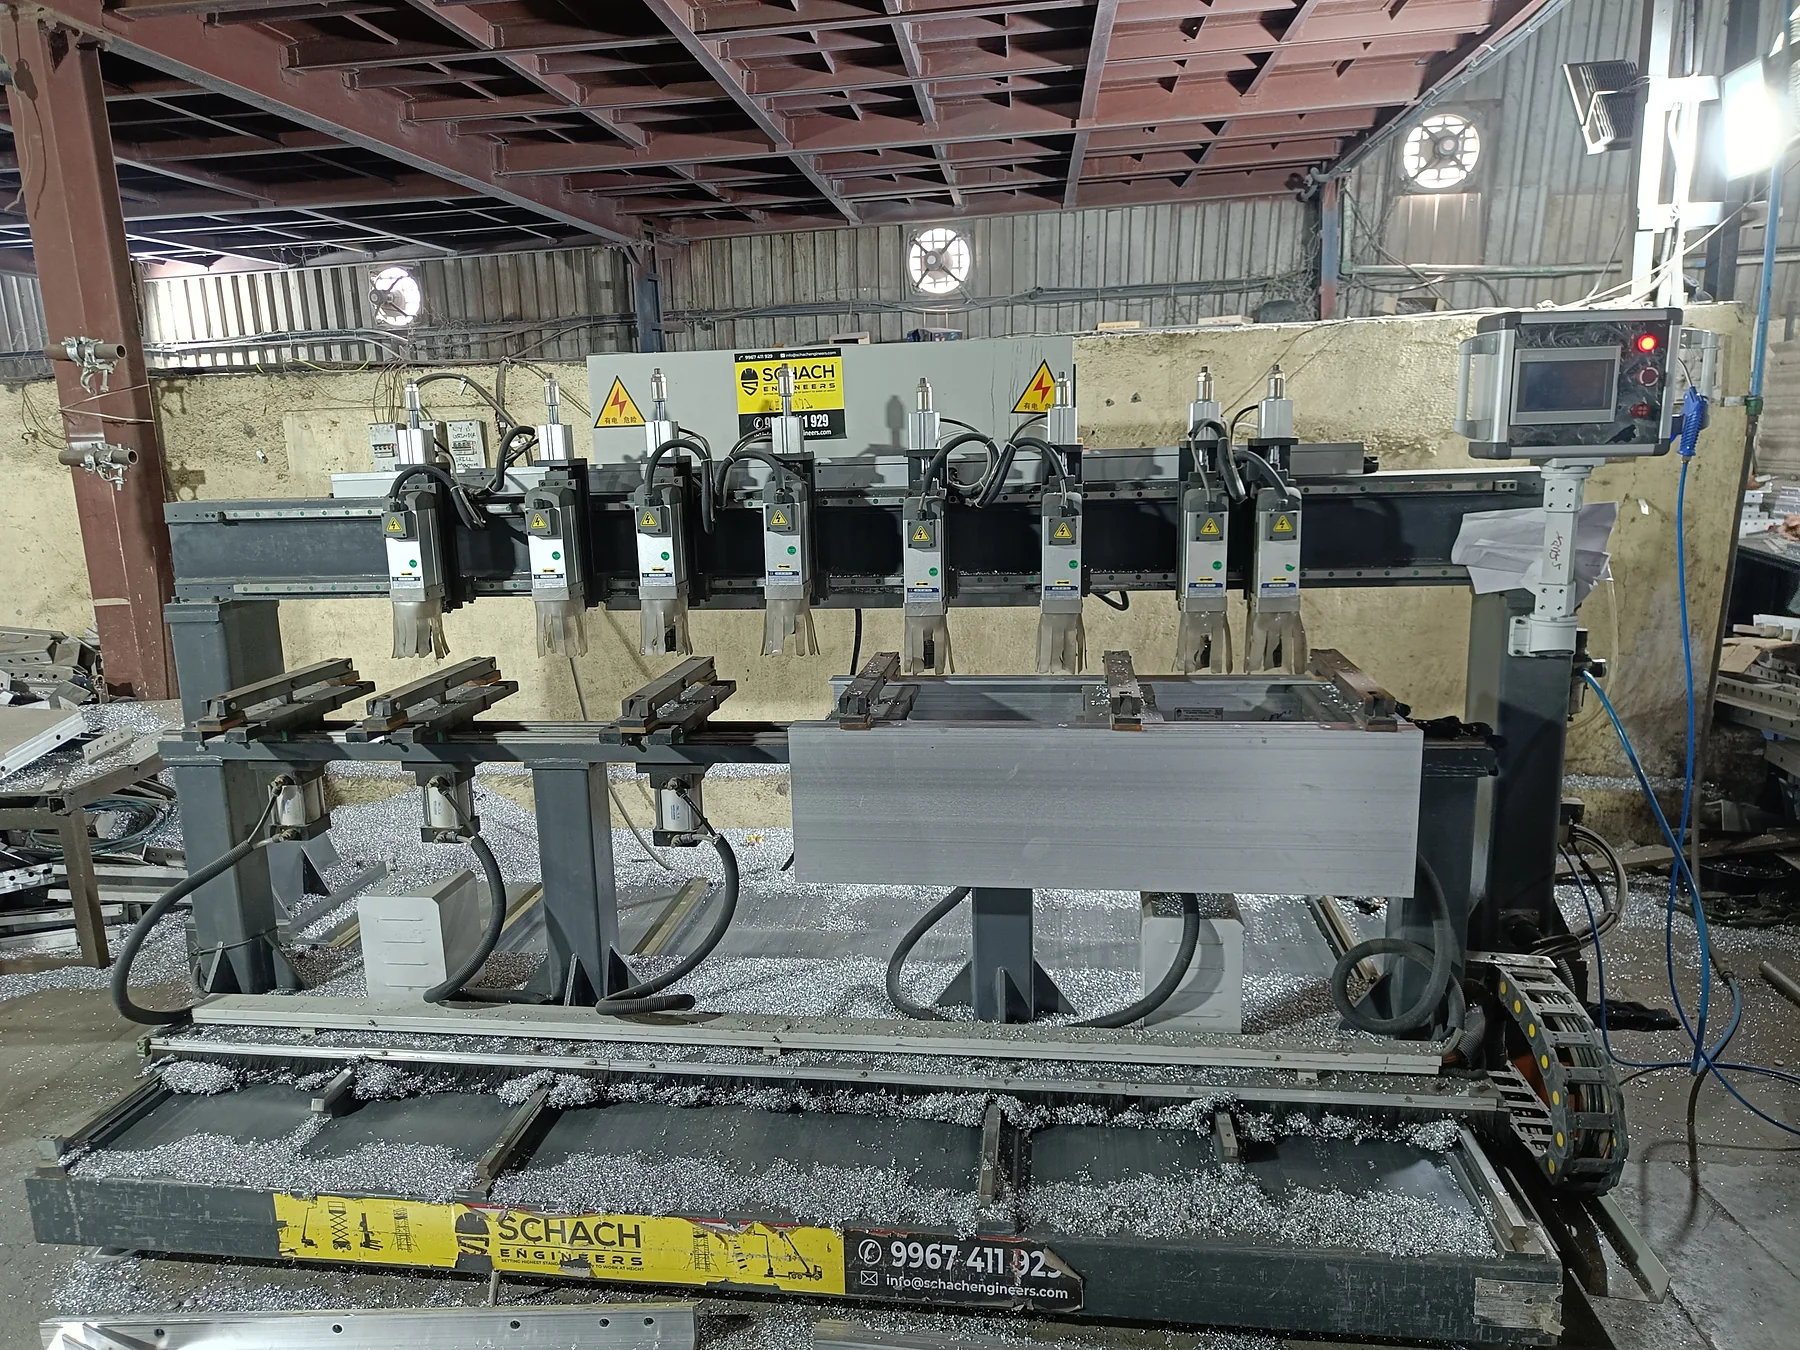
Multi-axis shearing, punching, milling, and press-shop operations against approved drawings.
Welding lines
Friction stir welding, fabrication fitting, full welding, and robotic welding where applicable.
Special fabrication
Dedicated work for staircases, curved elements, round columns, and project-specific assemblies.
Surface finishing
Grinding, cleaning, buffing, lacquering, priming, or painting according to the product system.
Controlled packing
Room-wise or unit-wise identification, pallet packing, packing lists, and coordinated dispatch.
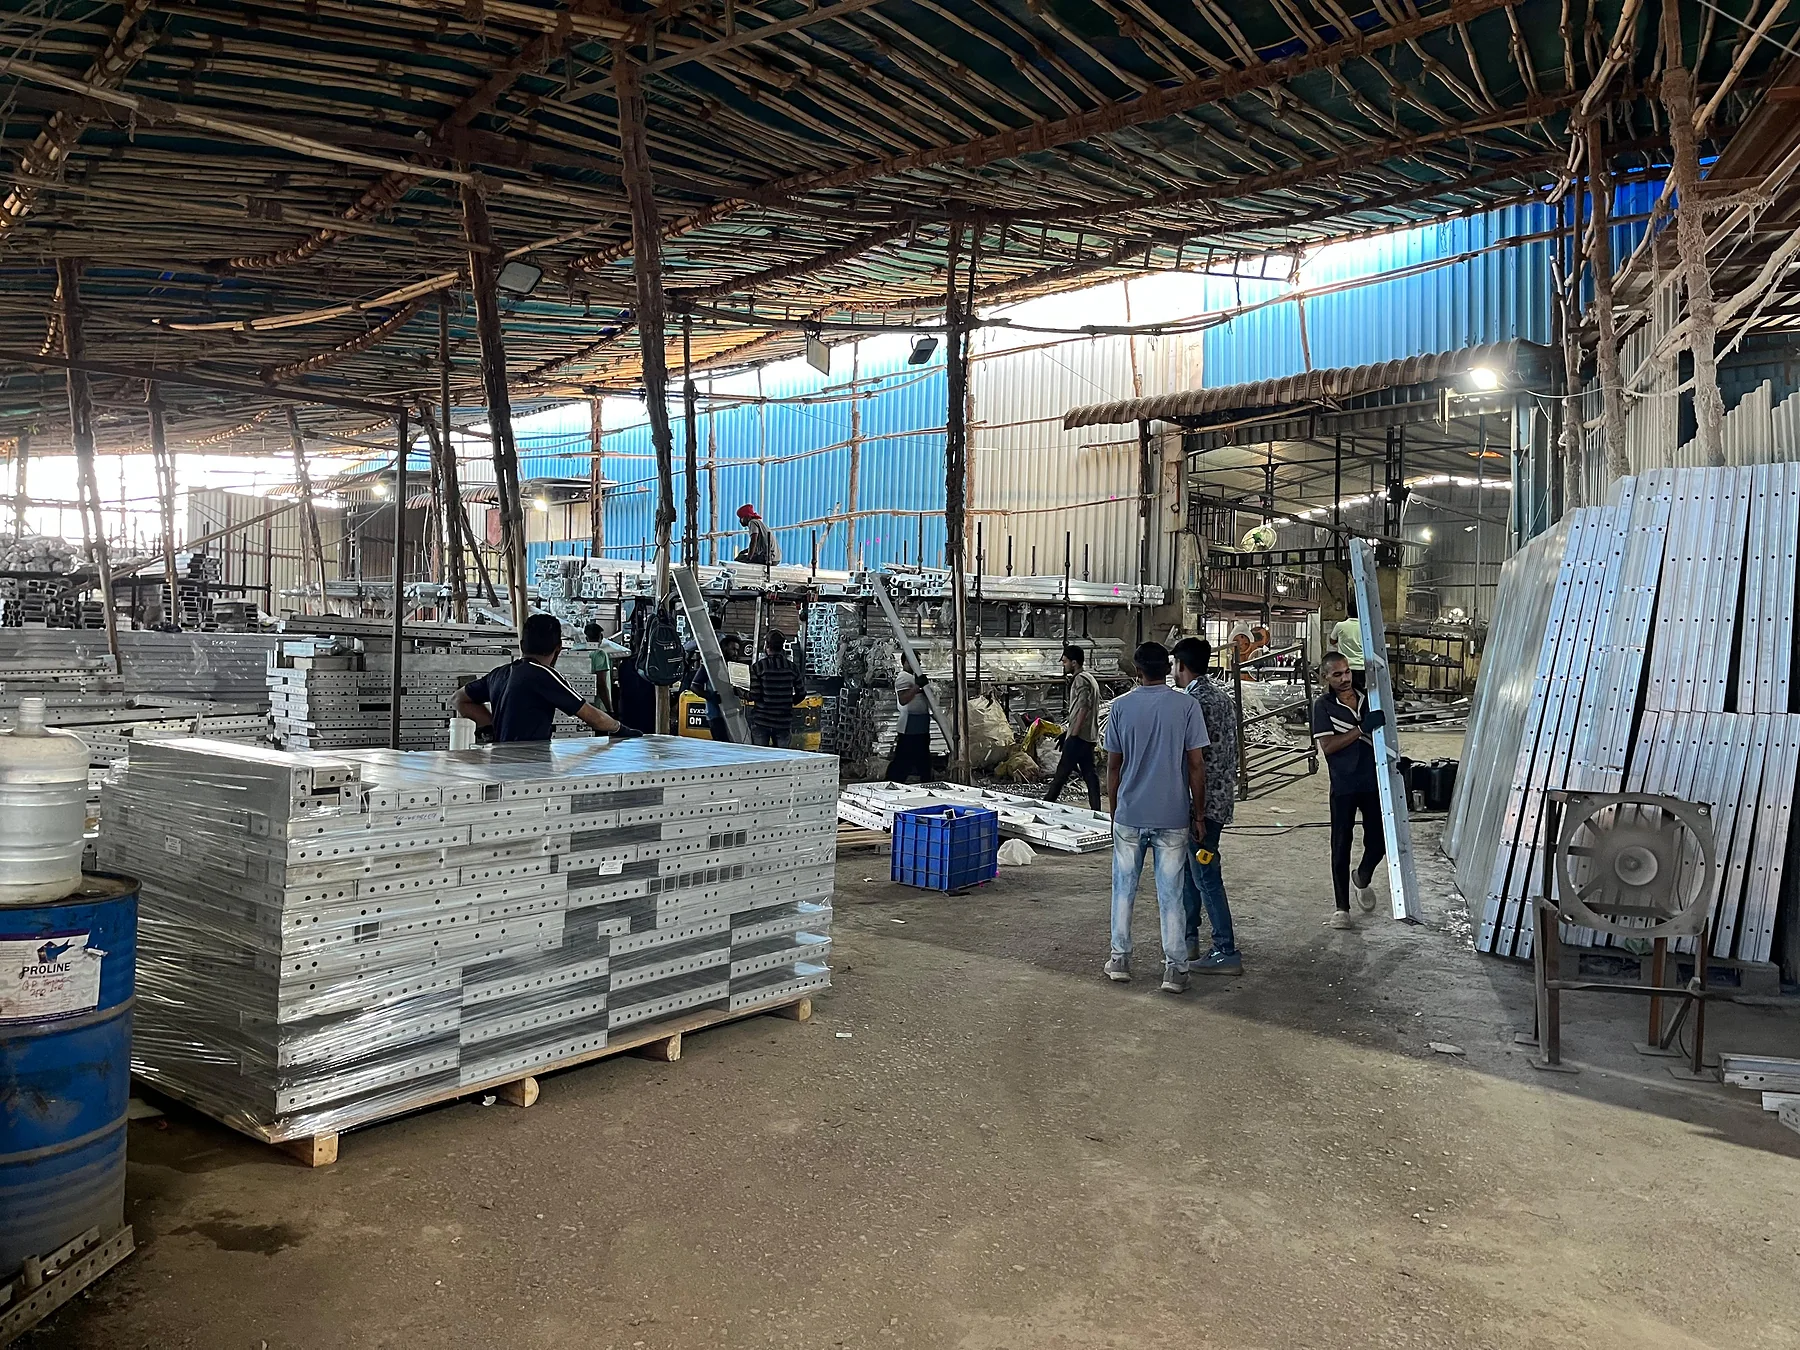
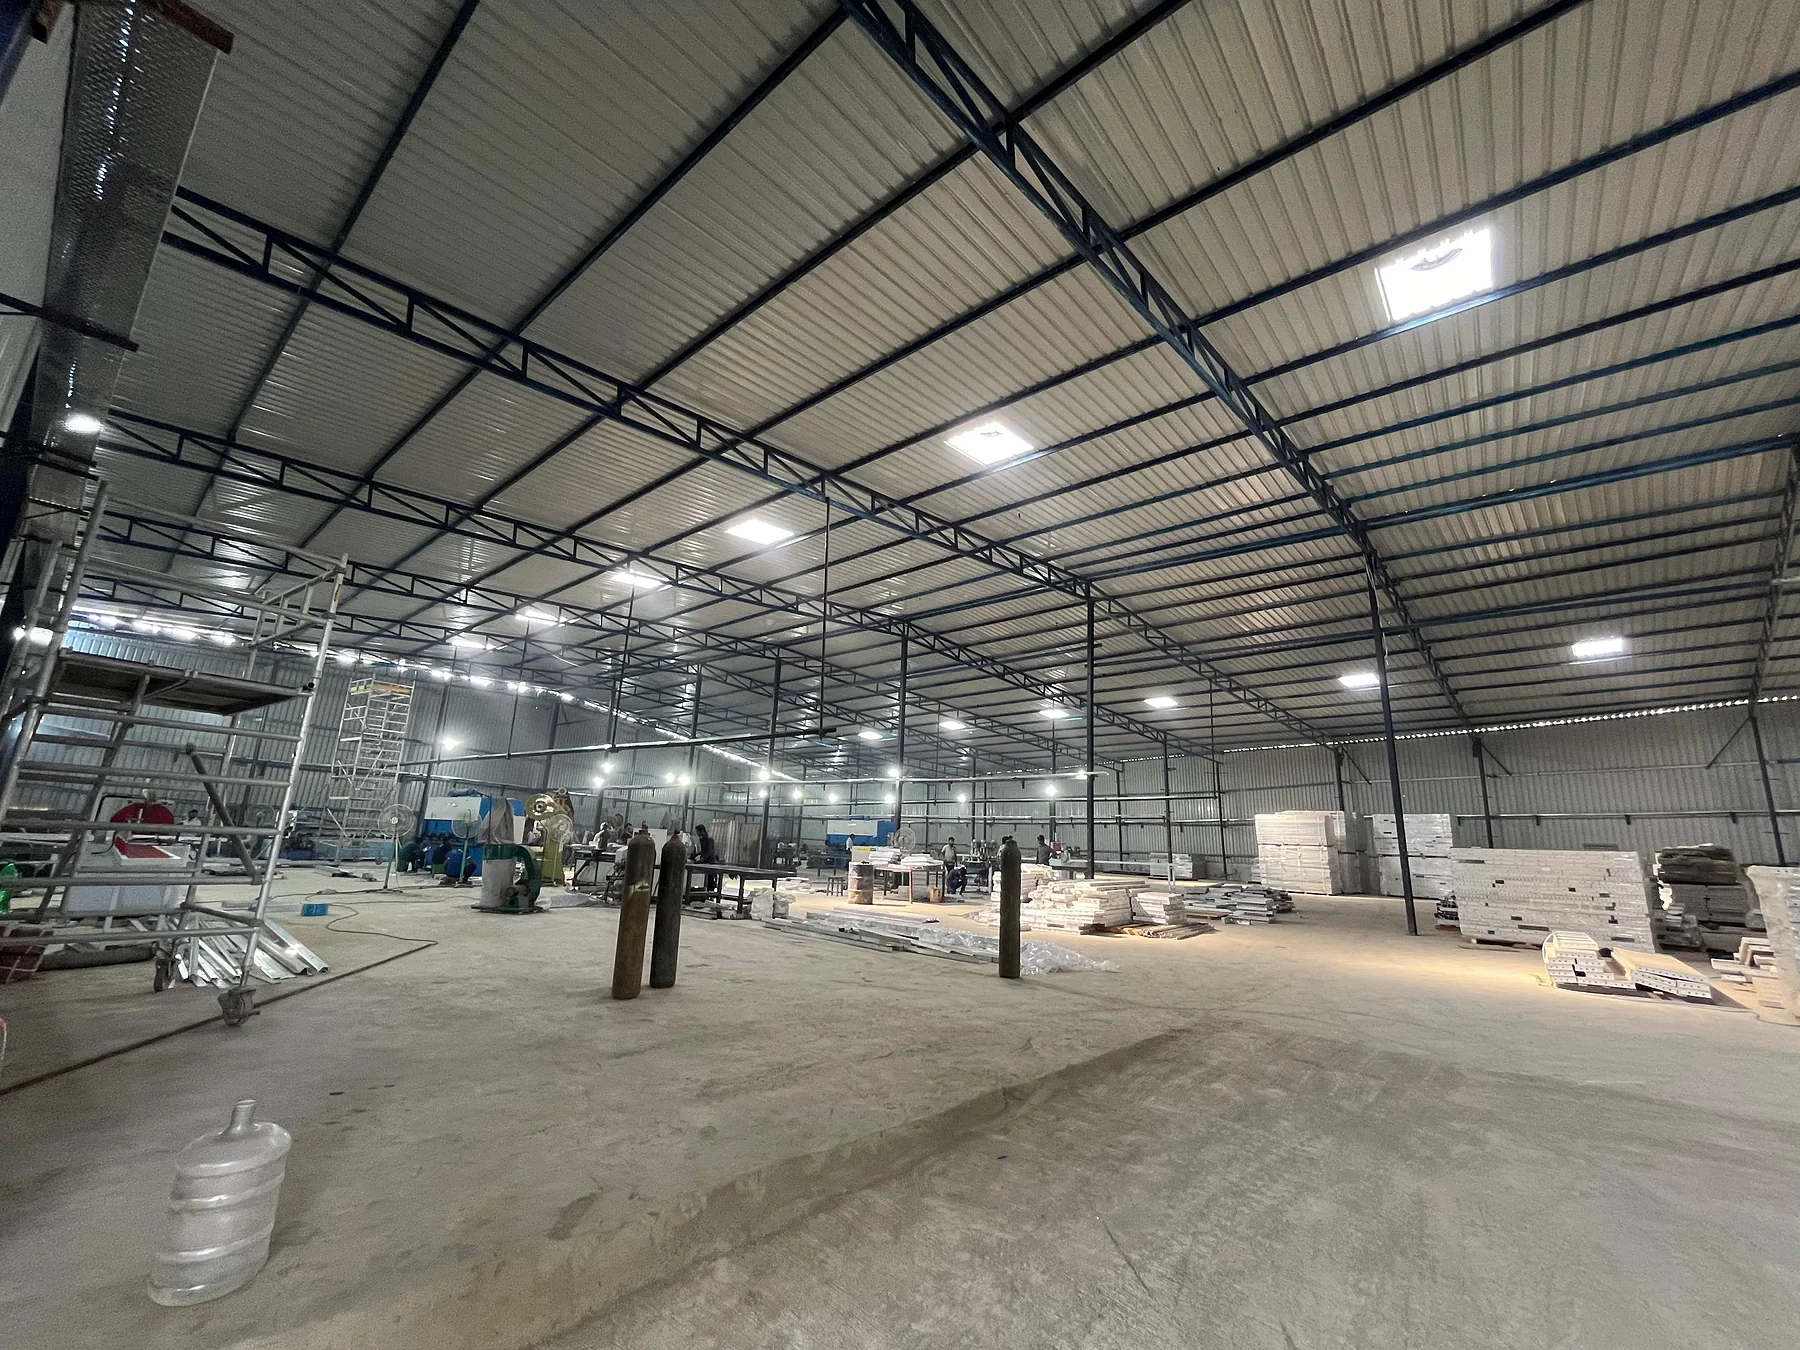
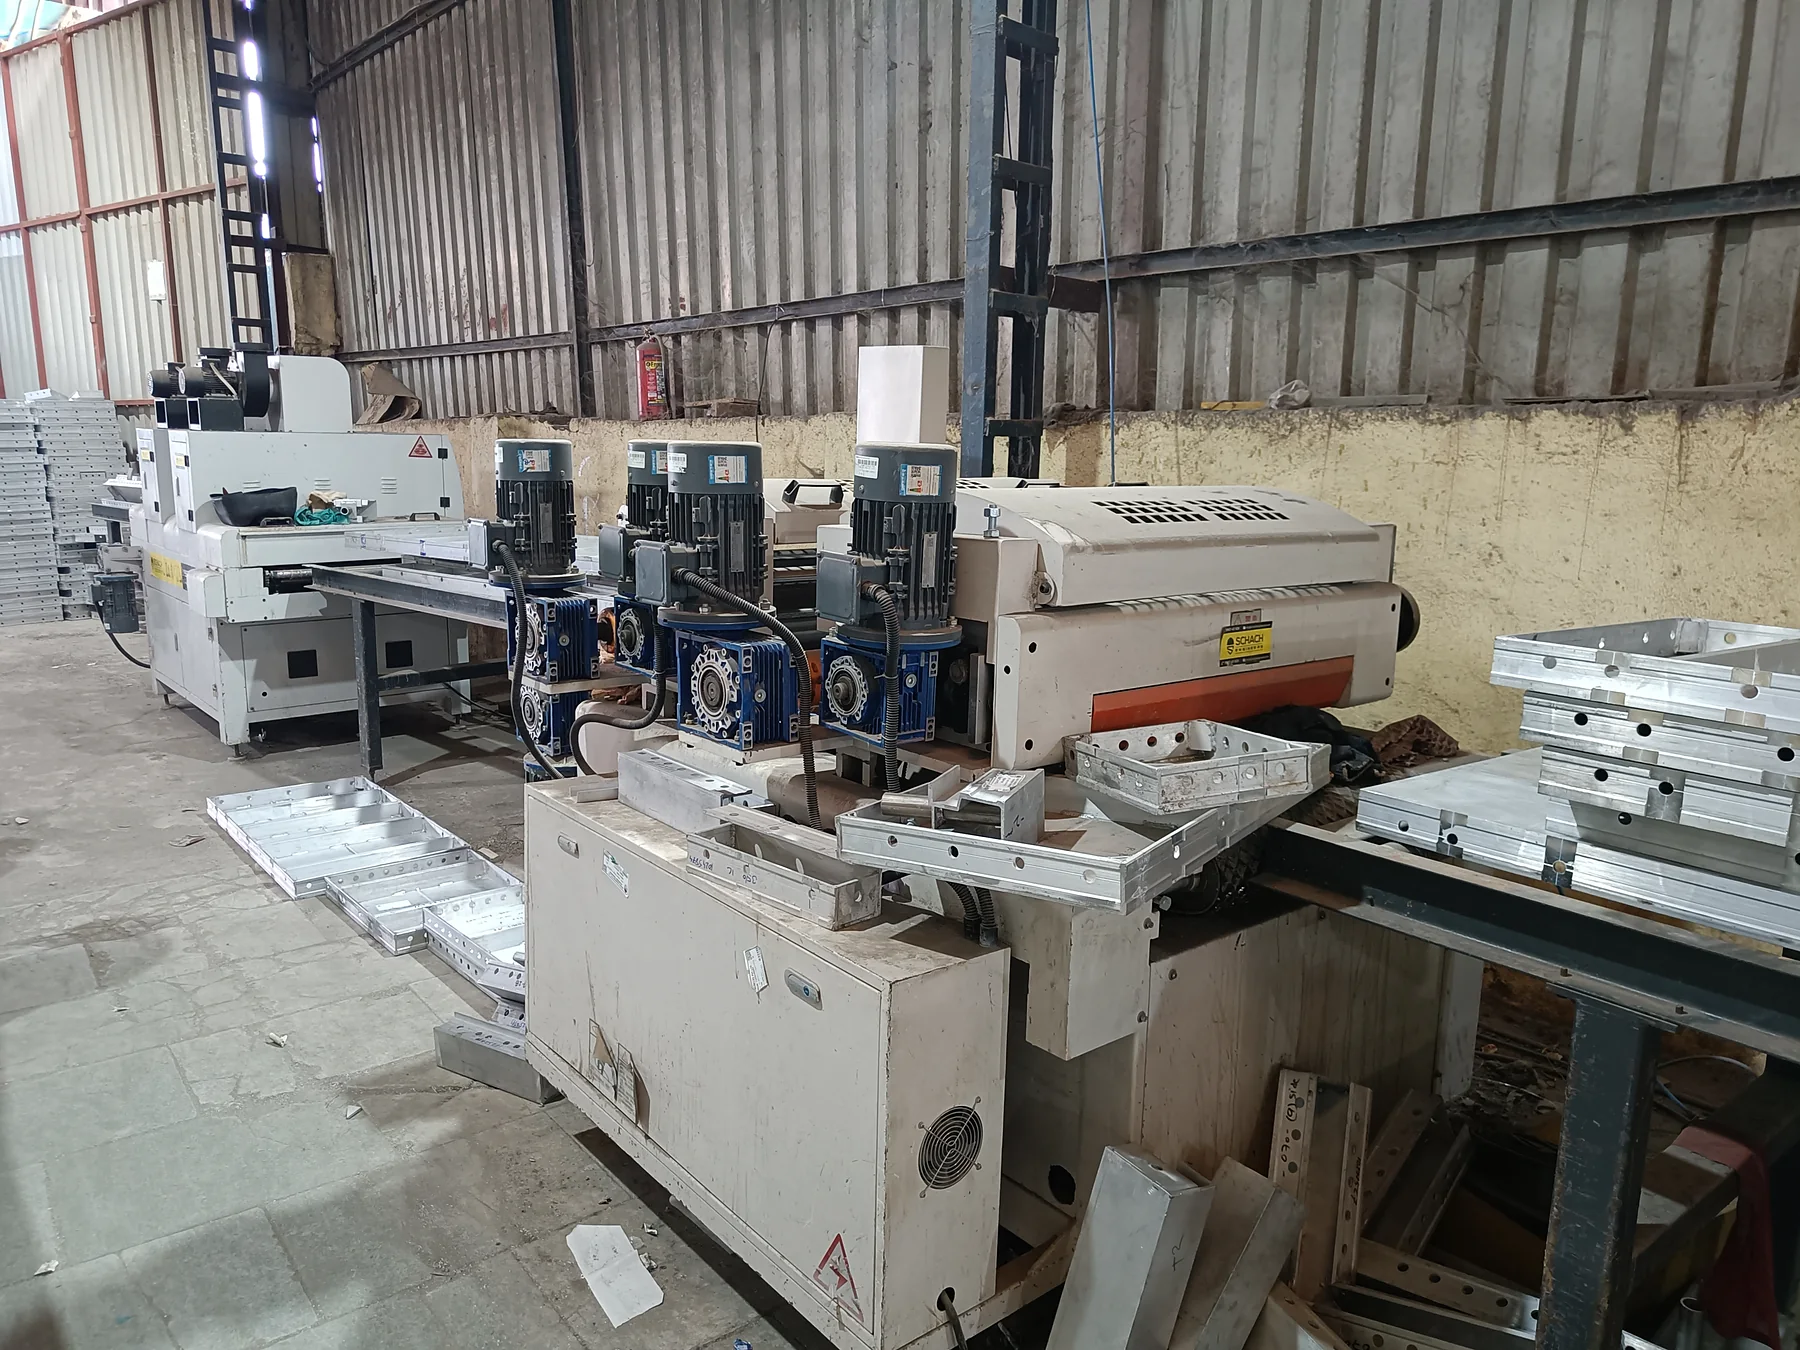
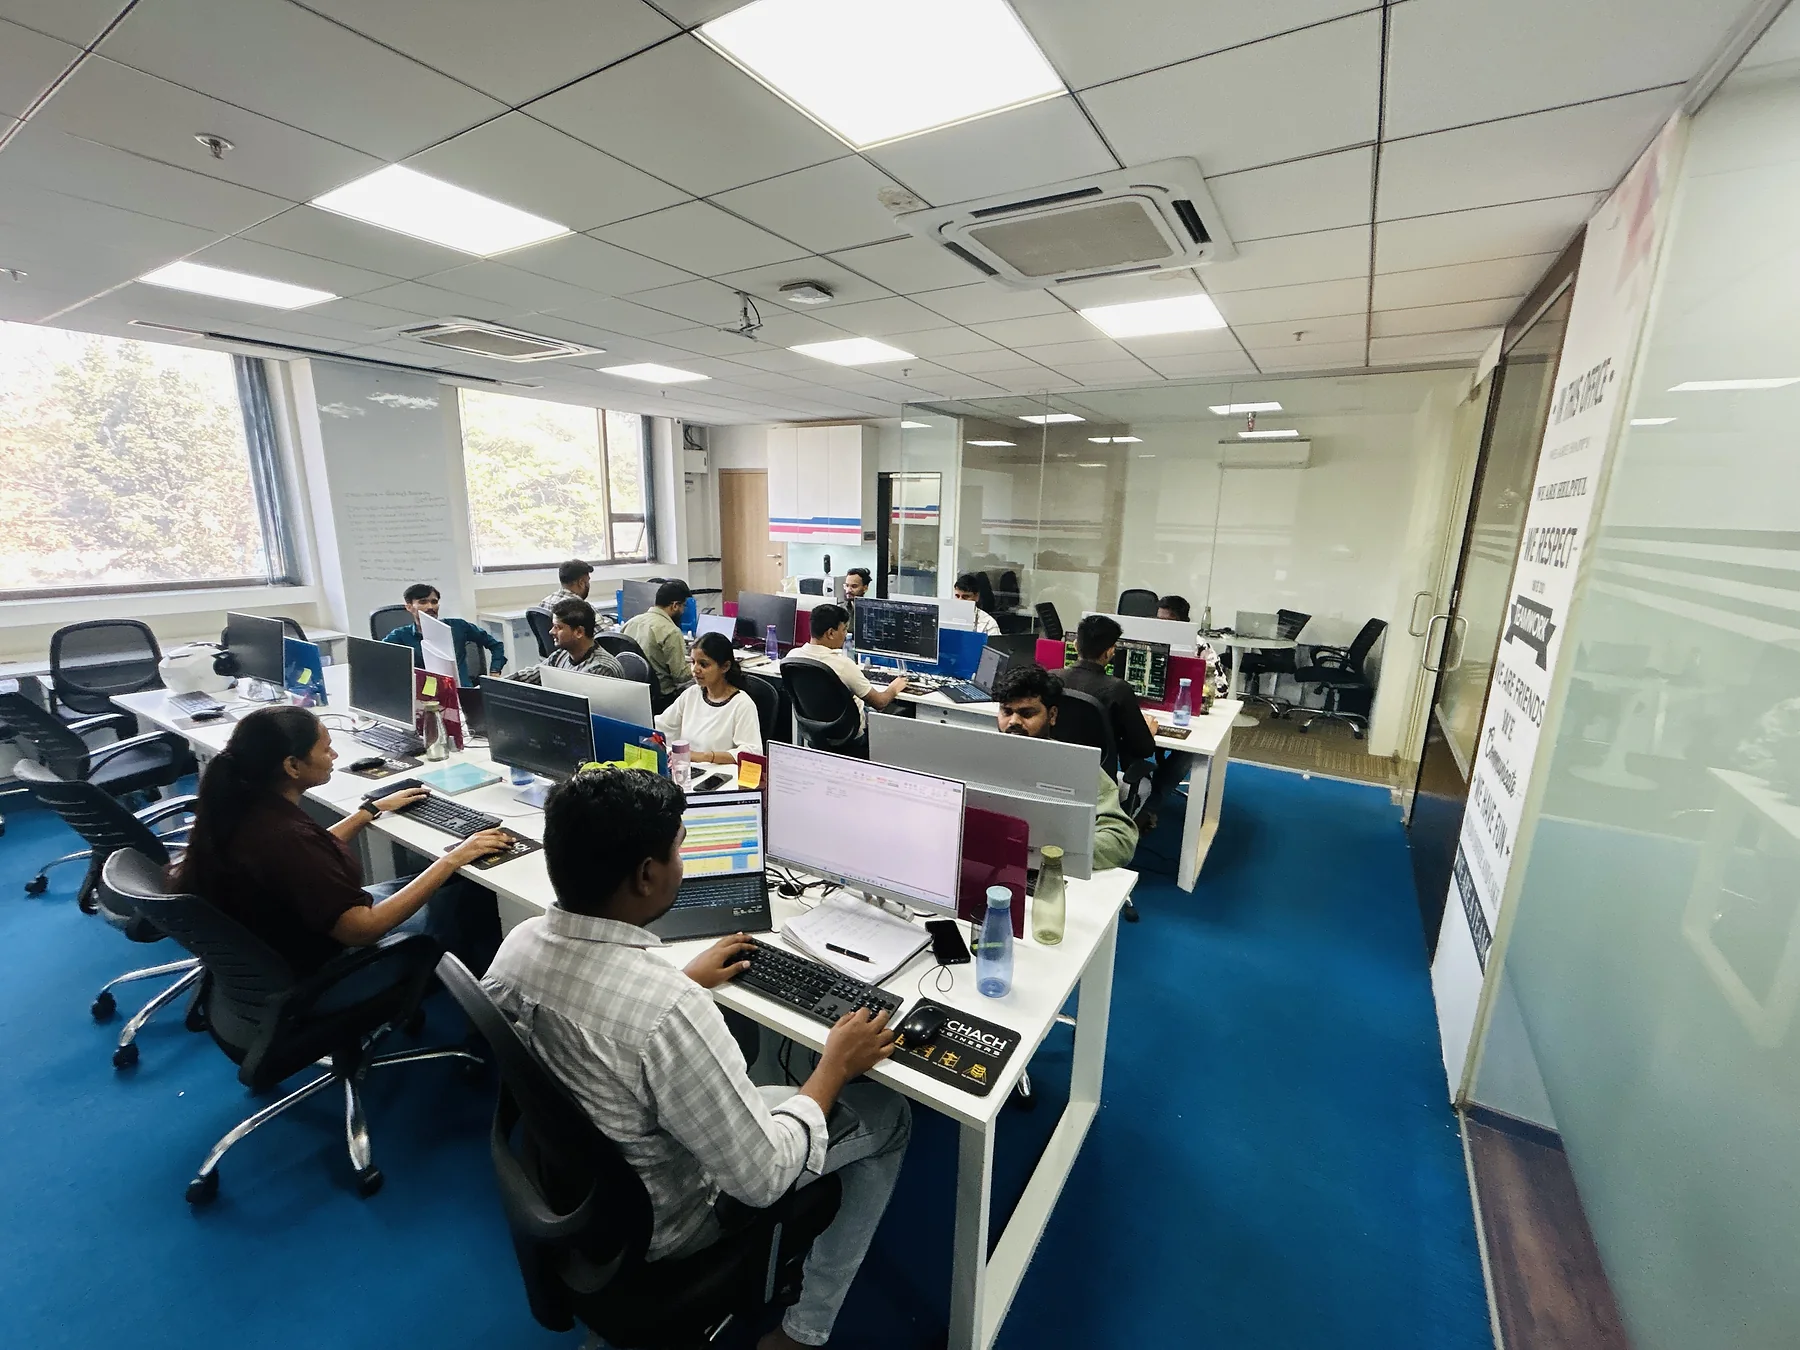
Equipment, people, and inspection connected on one floor.
Current factory photographs show the operations behind the documented workflow, from machine preparation and welding to finishing and engineering release.
Quality is checked at material, process, product, and site stages.
Material verification
Incoming dimensions and chemical properties are checked for each raw-material lot.
Traceable production
Unique barcodes support panel identification as material moves through production and packing.
Documented inspection
Components are checked against approved fabrication information, including a final 100% inspection.
Site verification
Scanning and installation checks help reconcile packed material with the planned site sequence.
In-house tooling keeps production responsive.
The toolroom supports new product development, process reliability, and fast correction when project requirements change.
- 01In-house jigs, fixtures, and production dies
- 02Tooling modification and process upgrades
- 03Root-cause analysis and production diagnostics
- 04Preventive and predictive maintenance
- 05Engineering-led quality and cost improvement
Documented systems, with product-specific certificates on request.
Schach Engineers is presented in its catalogues as ISO 9001:2015 certified by TUV Nord. Aluminium scaffold tower documentation references BS EN 1004 for applicable configurations. Project submittals and certificates depend on the selected system and scope.